Welder Certification — ISO 9606-1 Complete Guide
Introduction
EN ISO 9606-1 defines requirements for the qualification of fusion welders on steels. It is mandatory for most welded construction, pressure equipment (EN 13480, EN 13445) and steel structures (EN 1090).
---
Essential Variables
| Variable | Description |
|---|---|
| Welding process | 111, 131, 135, 136, 141, etc. |
| Joint type | Butt (BW) or fillet (FW) |
| Filler material group | FM1 to FM6 |
| Material thickness | Defines qualified range |
| Pipe diameter | Defines qualified range |
| Welding position | PA, PB, PC, PD, PE, PF, PG, PH, PJ, H-L045 |
| Weld details | Backing, root gas, etc. |
---
Qualification Range — Thickness (Butt Welds)
| Test piece thickness (t) | Qualified range |
|---|---|
| t ≤ 3 mm | t to 2×t |
| 3 < t ≤ 12 mm | 3 mm to 2×t |
| t > 12 mm | ≥ 5 mm (no upper limit) |
---
Testing
| Test | Mandatory | Description |
|---|---|---|
| Visual examination | Yes | Per ISO 17637 |
| Radiography or UT | Yes (BW) | Internal imperfections |
| Bend test (face + root) | Yes (BW) | Former 4t, 180° |
| Fracture test | Alternative | Alternative to bend |
Acceptance criteria: Imperfections within ISO 5817 Level B.
---
Validity and Prolongation
- Initial validity: 2 years
- Prolongation: Every 2 years via re-test, employer confirmation, or production welds tested in last 6 months
---
Practical Tips
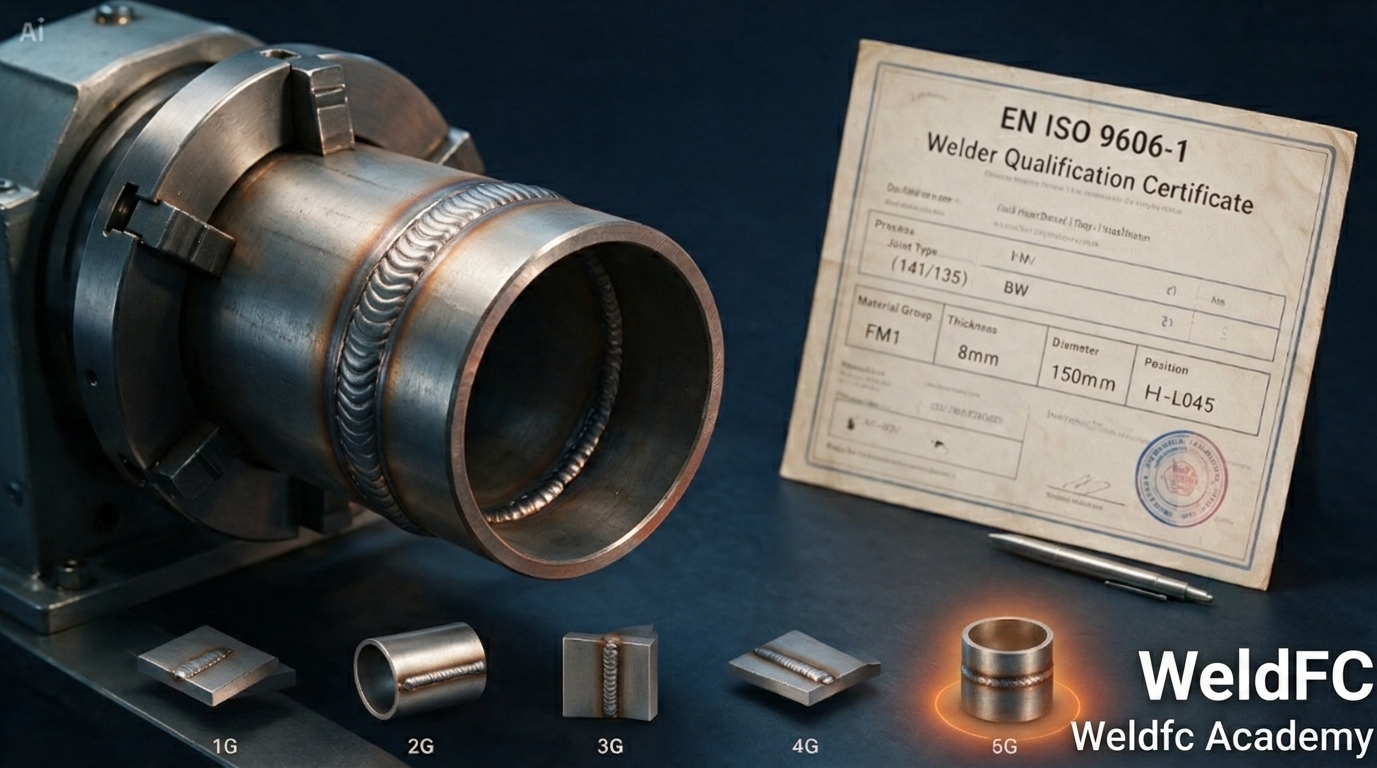
- H-L045 (6G) on pipe ≥ 150 mm = maximum coverage
- Multi-process (TIG root + MIG/MAG fill) = two qualifications from one test piece
- BW qualifies FW — always test on butt welds when possible
---
*Article based on EN ISO 9606-1:2013. Published on WeldFC Academy.*